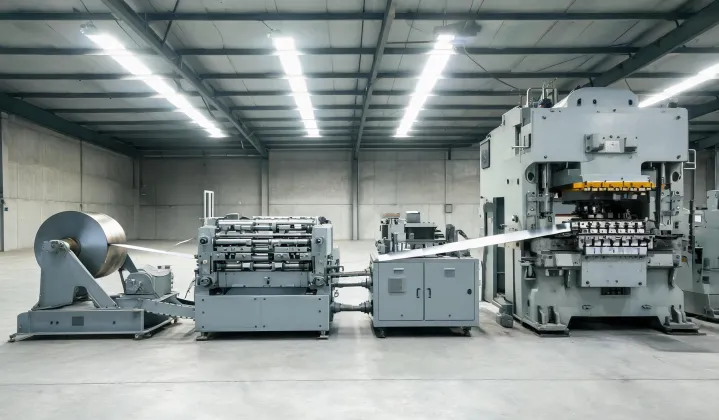
sheet metal stamping press

A sheet metal stamping press RFQ is shaped by the strip, the die and the feed window, not by a generic metalworking headline. State thickness, coil width, required load position in the stroke, and whether flywheel or servo energy covers the full stroke at the intended cycle. Upstream decoiler, straightener and feeder, plus downstream scrap and part handling, must be marked as included or plant-side. Representative production samples belong in the brief; a paper drawing alone does not prove feed pitch.

Coil-fed sheet metal stamping press with straightener and feeder

Operating duty

Operating context
Sheet-metal stamping cells that punch, form and trim coil or blanks. Press-brake bending, roll forming and hydroforming are adjacent processes and need a different brief. Work envelope, tooling mass and feed pitch must be written together.

Operating duty: Sample run

Run the intended strip through the production die. Record force at the rating point, working energy, stroke and the exact slide motion. If energy is short at the bottom of the stroke, a higher headline tonnage will not close the part. Read rating-point comparison.

Site readiness

Confirm coil-car or decoiler space, straightener loop, feeder pass-line height and scrap conveyor exit. Compressed air demand, three-phase supply and PLC interface names belong in the same note. Cooling water is only relevant if the quoted drive or lubrication unit requires it.

Owner acceptance

Inspect parts over an agreed run length. Record feed interruptions and recovery. Commissioning should verify agreed protective functions through competent personnel; a successful empty press cycle is not acceptance of the production cell.

Selection factors that change the sheet metal stamping press choice: coil yield strength, progressive-die length versus bolster, upper-die mass versus the listed kg limit, and whether transfer fingers or robots occupy the same work envelope. Positioning tolerance of the feeder pitch must match the die. Changeover between two strip widths may need extra straightener cassettes that a machine-only bid omits.

Limitations: we cannot convert a bending-brake RFQ into a stamping-cell quote by renaming the page. We cannot promise FAT dates. We cannot treat AIDA or any other published model table as stock we sell. Those pages name attributes such as rated force in kN, rating point, working energy, stroke, no-load SPM, die mass and bolster size; we use those names as buyer questions. Cycle time claims without material and lubrication are incomplete. If the application is insert work or a vertical press, say so; this page assumes a coil or blank sheet path.

Write the sheet-metal trial into the enquiry

Discuss Your Requirements